





Engineering Basis for Selection of Anticorrosion Coatings for Automobile Parts
When selecting corrosion protection coatings for automotive structural parts, fasteners and chassis components, engineers need to integrate the operating environment, substrate type, assembly clearance and life requirements into a single evaluation framework. Common failure modes include crevice corrosion, pitting and coating spalling, which are often caused not by a single factor, but by a combination of coating and substrate galvanic potential differences, surface preparation quality and subsequent assembly stresses. Taking ShowyMetal batch CNC machined automotive aluminum alloy brackets as an example, from 3-axis or 5-axis milling to final assembly, the matching degree of the coating system directly determines the survival rate of the parts in the wet heat cycle test.
Matching principle of substrate characteristics and corrosion mechanism
The corrosion potential of different metal substrates determines the chemical compatibility of the coating system. Aluminum Alloy (e.g. 6061-T6, 7075-T6) is prone to pitting corrosion, stainless steel (304/316) may experience stress corrosion in chloride ion containing environments, while carbon steel is primarily exposed to both uniform corrosion and localized electrochemical corrosion risks. For high finish surfaces with Ra less than 0.8μm, physisorption coatings are more prone to peel off, while chemical crosslinking coatings tend to achieve better mechanical bite for micro-convex surfaces with Ra ranging from 1.6μm to 3.2μm.
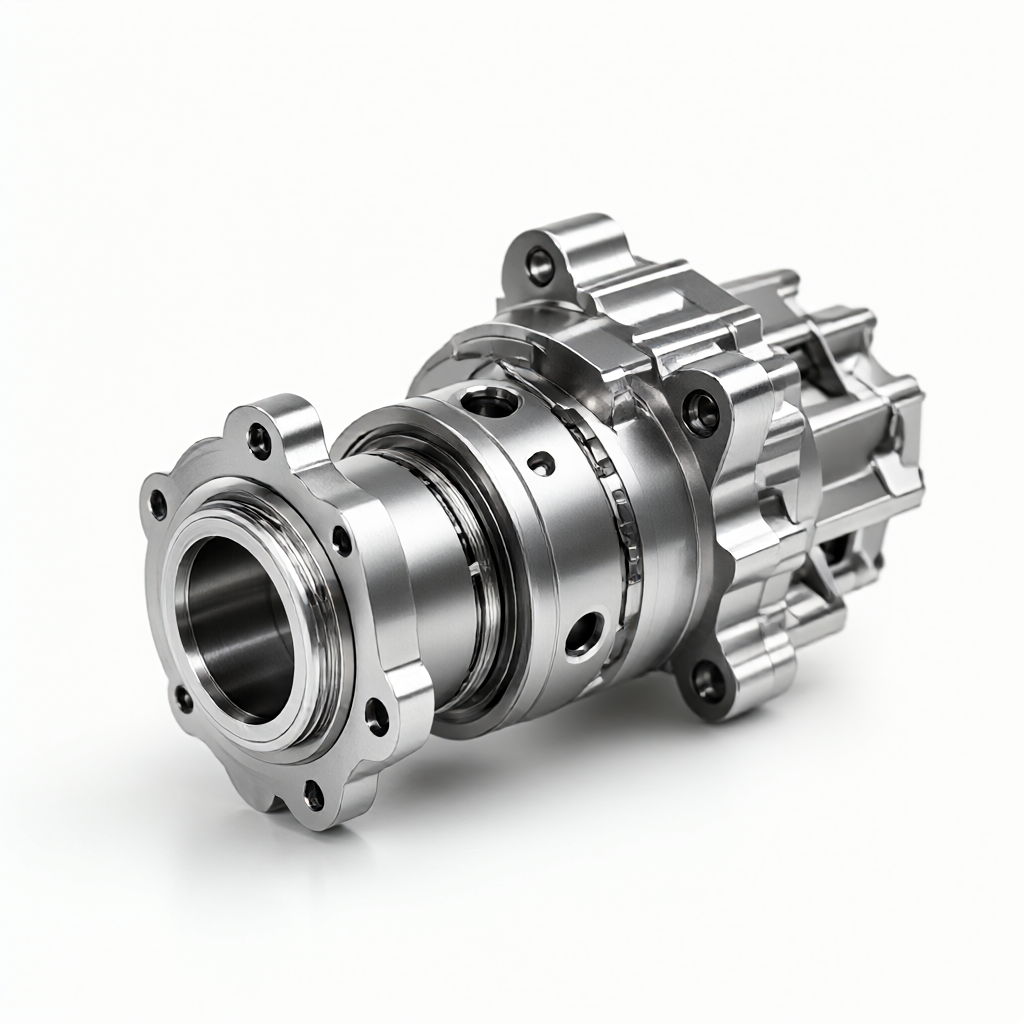
- Aluminum alloy:Cathodic protective coatings are preferred, or anodic oxidation plus sealing is used to prevent aluminum oxide films from dissolving in alkaline environments.
- Stainless steel:Avoid using conductive coatings with excessive potential difference from stainless steel to prevent the formation of galvanic cells to accelerate substrate corrosion.
- Carbon steel/alloy steel:Make sure the bottom layer has passivation ability or high thickness insulating layer to block the penetration path of water vapor and oxygen.
Comparison and Analysis of Main Corrosion Protection Coating Schemes
In actual mass production, electroplating, anodizing, powder coating and immersion treatment are the four main paths. Each scheme has significant differences in corrosion resistance level, appearance requirements, process complexity and batch consistency. The following is a comparison of process parameters and applicable scenarios for common automotive parts:
| coating type | Typical thickness/film characteristics | Salt spray test tolerance time | suitable substrate | mainly limited |
|---|---|---|---|---|
| Dacromet/Freco (mechanical plating + dip coating) | 10-20μm, flake zinc/aluminium layer | Usually 500-1000 hours (depending on class) | Carbon steel, galvanized steel, some aluminum parts | Single color, non-conductive, high temperature decomposition may produce odor |
| Aluminum anodization (including sealing) | 10-25μm oxide film | Usually 48-96 hours (weak neutral salt spray resistance, but good heat resistance) | Aluminum alloy (6061, 7075) | For aluminum only, no cathodic protection |
| Powder spray (polyester/epoxy) | 60-120μm insulating paint layer | Usually more than 1000 hours | Steel, aluminum, some engineering plastics | Large thickness, not suitable for precision mating surface; appearance needs to be flat substrate |
| Electroplating (zinc/nickel plating) | 5-15μm metal layer | Usually 48-96 hours (zinc plating); nickel plating has lower corrosion resistance but abrasion resistance | Steel, copper alloys, some aluminum | Hydrogen embrittlement risk (high strength steel needs hydrogen removal), appearance gloss fluctuates with process |
From a purchasing perspective, powder coating is not suitable for parts requiring conductive grounding due to thick insulation layers; while Dacromet has stable corrosion resistance, its matte appearance is difficult to meet the needs of high-end vehicles for mirror or high gloss finishes.
The decisive influence of surface pretreatment on coating life;
The early failure of many batch orders is not due to the coating material itself, but to inadequate surface pretreatment. Cutting fluid, trace metal chips and oil stains often remain on the surface of parts after CNC machining. If these contaminants are not completely removed, they will form Micro-corrosive batteries under the coating. Standard pretreatment processes should include degreasing, acid or alkali washing (depending on the substrate), water washing and passivation.
- Degreasing:Alkaline and non-saponified formulations are used and temperatures are controlled at 50-70°C to ensure removal of all organic residues.
- Passivation/conversion film:For steel parts, phosphating or silane conversion film thickness control in 3-5μm, can improve the adhesion of subsequent coatings to 5B class (ruled method).
- Aluminum processing:After alkali washing oxide scale, chromate or chromium-free passivation is carried out to form a corrosion resistant bottom film.
In batch production, consistency of pretreatment is more critical than single point treatment. If the surface condition of parts produced by 72 CNC machines fluctuates greatly between batches, the coating process must be equipped with online film thickness monitoring and adhesion sampling to offset the risk caused by pretreatment differences.
Design considerations for corrosion protection under tolerances and assembly clearances
Automotive parts often have tight assembly gaps, such as bearing seats and flange joints. In these areas, coatings are prone to assembly stress cracking or edge peeling, forming crevice corrosion channels. The design stage should require coatings to maintain a minimum continuous film thickness at sharp corners or thin walls. It is generally recommended that the coating thickness at sharp corners be no less than 5μm to avoid cracking caused by stress concentrations. For precision mating surfaces with tolerances within ± 0.01 mm, coatings must be extremely thin or erodible to avoid cumulative thickness leading to assembly interference.
In addition, polyhedral parts machined by 5-axis milling have cavities and blind hole areas that are difficult to cover by conventional spraying and require immersion or vacuum-assisted spraying. If the part contains sealing threads or O-ring grooves, the coating should avoid invading the sealing surface, otherwise it will affect compression ratio and resilience, resulting in sealing failure rather than corrosion failure.
Inspection standards and batch consistency control
Corrosion resistance cannot be judged visually alone, but must rely on standardized quantitative testing. Common methods include:
- Neutral Salt Spray Test (NSS):Follow GB/T 1771 or ASTM B117 and record the time to first blister or rust, not just the total time.
- Cyclic corrosion test:Simulating actual working conditions, combined with damp heat, salt spray and drying cycle, can reflect the real failure mode better than single salt spray.
- Adhesion Test:Grading method (ASTM D3359) to reach 0B-1B grade, or pull method to reach a certain MPa value.
- Film thickness detection:Using eddy current meters (non-ferrous substrates) or magnetic thickness gauges (non-magnetic substrates), measure at multiple points in critical areas to ensure no local over-thinning.
ShowyMetal performs full size inspection and visual sampling before batch shipment, equipped with coordinate, optical measurement and roughness meter. For corrosion resistant coated parts, additional film thickness distribution map and salt spray sampling report are added to ensure that the corrosion resistance fluctuation of each batch is controlled within SPC limits.
Common Failure Modes and Avoidance Strategies
Coating blistering and bulging
Usually caused by moisture on the surface of the substrate is not dry or the sealing is not strict. Avoidance scheme: set sufficient flash time after pretreatment, or use hot air circulation drying; for anodized parts, ensure that the sealing water temperature is above 95°C and the time is sufficient to saturate the film layer to prevent subsequent moisture infiltration.
Edge peeling and scratching
It mostly occurs in the assembly friction area or transportation collision. Avoidance scheme: increase the coating hardness in the key friction area, or adopt the wear-resistant coating system; increase the antistatic and cushioning measures in the packaging to avoid mechanical damage in batch handling.
crevice corrosion penetration
This occurs when the coating breaks down and seeps into the bottom of the crevice. Avoidance: increase the overlap area at the edges of the coating during the design phase, or additionally seal the crevice area prior to assembly to block the electrolyte flow path.
Conclusion and inquiry suggestions
Choosing the right corrosion protection coating is essentially a balance between substrate, process, environment and cost. For mass customization of automotive parts, it is recommended that engineers define corrosion resistance levels, appearance requirements and assembly clearance limits at the drawing stage so that manufacturers can accurately match the process route. ShowyMetal provides one-stop service from CNC machining, surface treatment to inspection and shipment. It has 3/4/5 axis milling, turning and milling compound and various coating processing capabilities. The accuracy can reach ±0.01mm and the surface finish Ra0.4μm. If you have specific part drawings or corrosion index requirements, welcome to send technical documents for feasibility evaluation and quotation, we will provide you with customized coating solutions in combination with batch consistency control requirements.
Common technical problems of corrosion protection coating
CNC machining aluminum alloy bracket after anodizing can also be plated?
Not recommended. Anodizing forms a porous film that prevents the plating solution from contacting the substrate, resulting in poor adhesion and uneven thickness of the electroplated layer. If plating is required, it should be completed before anodizing, or replaced by an insulating coating such as powder spraying.
Does dacromet coating affect electrical conductivity of parts?
Yes, Dacromet is an insulating coating that significantly increases contact resistance. If the part is used for grounding or conductive paths, select local film removal or conductive coating, and consider conductive compensation measures in the design.
How to ensure the consistency of coating color between batches in batch production?
The key lies in the standardization of curing temperature and time, and the locking of powder batch number. Using online colorimeter sampling, and controlling the color difference within ΔE less than 1.5, can effectively reduce the visual difference between batches.
Does the salt spray test 500 hours qualified represent actual use without corrosion?
Not directly equivalent. Salt spray test is accelerated simulation, actual corrosion resistance is also affected by assembly stress, local damage and environmental chloride ion concentration. It is recommended to combine cycle test with long-term outdoor exposure/freeze-thaw test to comprehensively evaluate life.
How much should the coating thickness of precision mating surface be controlled?
Usually 5-10μm on one side is appropriate to avoid cumulative thickness exceeding the fit gap. If the tolerance is less than 0.05mm, it is recommended to use thin layer plating (3-5μm) or electroless nickel plating, and cooperate with oil-free assembly process to prevent stagnation.
